
 English
 French
 German
High Temperature Bearings. What Changes in the Heat
Heat Zone Walkthrough
High temperature bearings are not a separate product line. They are the same rings, balls and cages built with a clearance group, a grease and a seal that hold up in the heat your process makes. This guide walks your equipment by heat zone, from warm to the hot spot, and says what changes inside the bearing at each step.
A bearing that runs smooth on the bench can be rough in a month beside an oven. Nothing was wrong with the part when it went in. The heat changed the running gap, cooked the grease and softened the cage.
Most positions on a bakery line, a heat tunnel or a dryer still take a plain deep groove ball bearing. The question is which build of that bearing you order. The answer starts with knowing how hot the seat really runs.
What Heat Actually Does to a Bearing
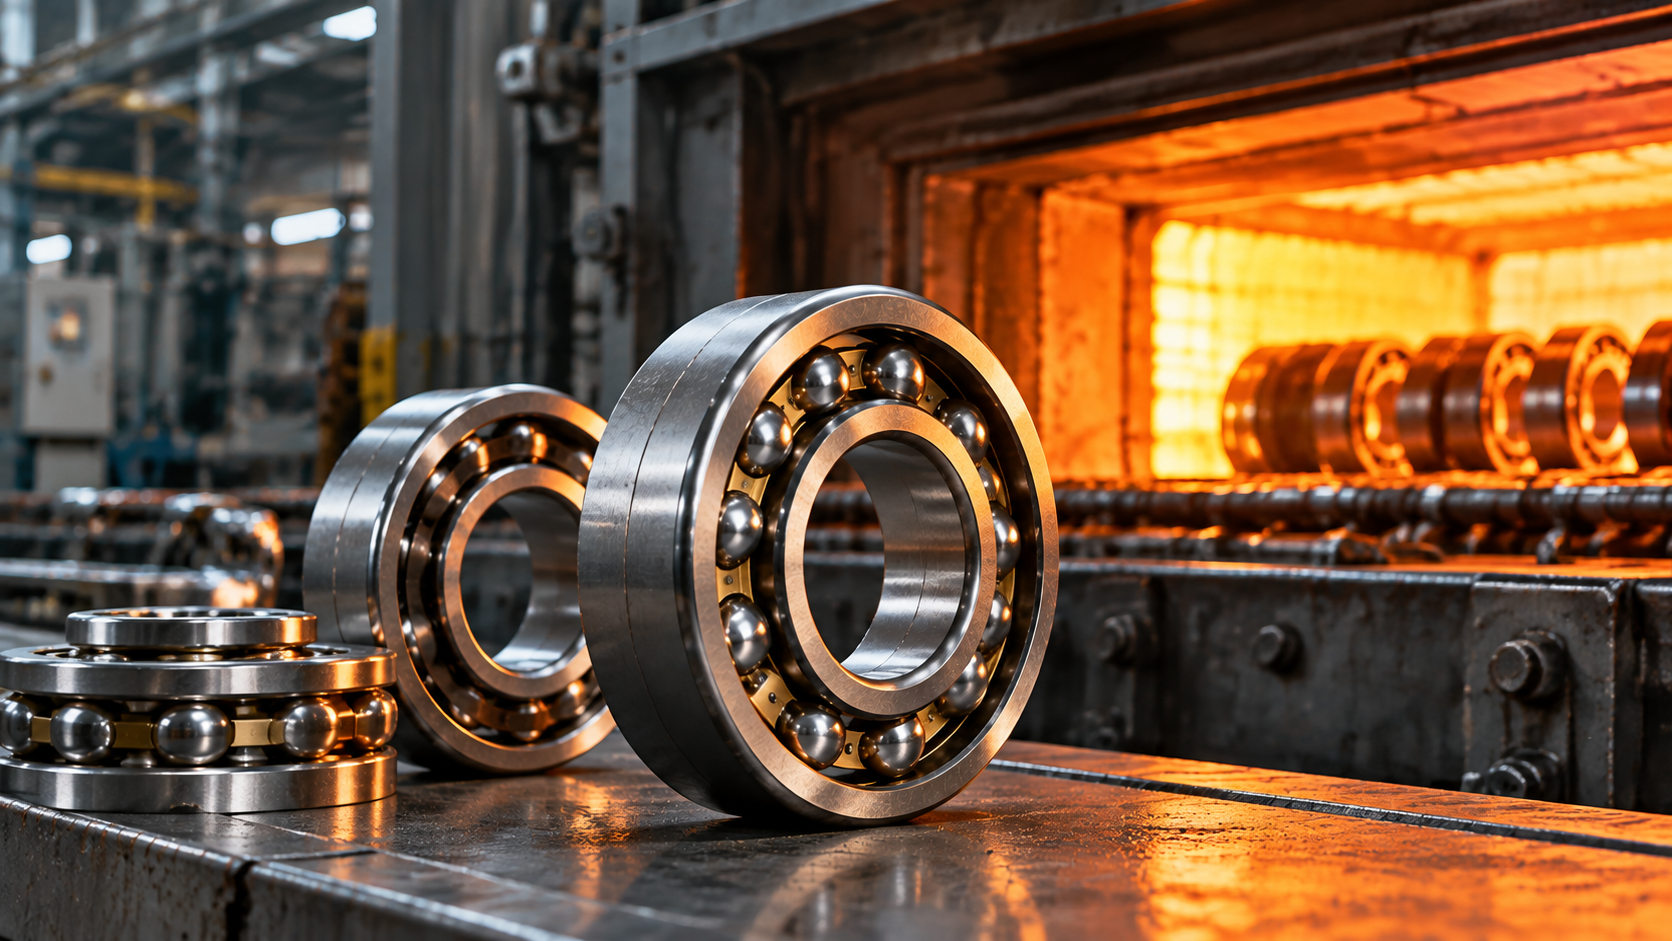
Four things change once a bearing sits in a warm place. They happen at the same time, and whichever bites first decides how the part fails.
1The clearance closes. Clearance is the small gap between the rolling elements and the raceway. The inner ring runs hotter than the outer ring, so it grows more, and that gap shrinks.
2The grease ages faster. Heat pushes the oil out of the thickener and cooks off the light part of it. What is left is dry soap, and the bearing runs metal on metal.
3The cage softens. A moulded polyamide cage is good to about 120 degrees C. Past that it loses stiffness, and a soft cage lets the balls wander out of line.
4The seal hardens. A contact seal is a rubber lip pressed against the ring. Heat takes the spring out of it, so it either drags or stops sealing at all.
Where the Heat Comes From
The process is the first. An oven wall, a kiln, a dryer drum or a heat tunnel throws heat straight into the housing. Here the bearing is a victim of the equipment around it.
The motor is the second. A motor that runs warm soaks its own bearings, and a bearing heated from the inside is a different problem from one heated from outside. It usually needs a look at the motor, not a harder bearing.
Friction inside the bearing is the third. Too much preload, a tight fit or a starved raceway all make the bearing heat itself. Fix that cause first, or better hardware will not help.
Zone One, Warm Equipment
Zone one is equipment that feels warm to the hand but not hot enough to hurt. If the housing sits under 100 degrees C in normal running, the heat is mild and a standard bearing usually copes.
At this level the standard CN clearance group still works, and a normal NLGI grade 2 grease holds its place. The ring grows, but not enough to close the running gap.
What Still Works in Zone One
Keep the everyday sizes. A 6004 at 20 x 42 x 12 mm is rated 9.36 kN dynamic and 5.10 kN static, and a 6204 at 20 x 47 x 14 mm carries 12.8 kN dynamic and 6.55 kN static. Both are fine in warm air when the grease is fresh and the fits are right.
Zone Two, Hot Equipment
Two things change in the order. The clearance group moves up to C3 or C4, because the extra cold gap pays for the growth that happens at running temperature. The grease has to match the temperature at the seat, not the temperature of the room.
A metal shield usually beats a contact seal here. It keeps dirt out without a rubber lip pressed against a hot ring. Our notes on bearing internal clearance cover how C3 and C4 groups are picked.
An application review, not a guess. Send the temperature the equipment actually reaches at the bearing seat, plus the duty cycle, and we will reply with the clearance group, cage, grease and seal we would supply. Trial parts are available before a production run. Start with a short message and describe the position.
Zone Three, The Hot Spot
The Cage Sets the Ceiling
A moulded polyamide cage is good to about 120 degrees C. That is the practical ceiling for the common build, and it is a cage limit rather than a steel limit. Past that point, ask for a steel or brass cage. The rings and balls will take far more heat than the moulded cage can.
The Grease Goes First
Grease usually gives up before the steel does. Heat drains the oil out of the thickener, and once the oil is gone the raceway runs dry. That is why a hot position needs a grease chosen for the seat temperature, and why the relubrication window gets shorter. More detail sits in our article on deep groove bearing grease.
When Stainless or Ceramic Wins
Two upgrades change the picture. Stainless rings and balls resist heat and corrosion together, so they suit a wash-down bakery or a damp dryer. Ceramic balls take the hottest positions and also cut the electrical path that causes shaft currents in a motor. The trade-offs are set out in ceramic vs steel ball bearings.
Clearance Groups and Heat
Clearance is measured on a cold bearing, because a cold bearing is the only one you can measure. That number is spent the moment the machine comes up to temperature. The inner ring, warmed by the shaft or the process, grows a little more than the outer ring, and the gap you measured disappears.
This is why a hot housing takes a C3 or C4 group and not a CN. It is not a loose bearing. It is a bearing with the gap it will need once it is hot.
Seals in the Heat
The seal is the part most often overlooked on a hot line. A contact seal has a rubber lip that rides on the ring, and heat takes the life out of that lip. It hardens, stops following the ring and starts to drag.
A metal shield has no rubber and no spring to lose. It keeps its shape in the same heat and still blocks coarse dirt, which is why it is the safer pick on a hot position that stays fairly clean.
On a clean hot line, an open bearing with the right grease is often the best answer of all. Nothing wears and nothing has to flex. Where the position also sees wash-down or grit, a 2RS seal keeps it out, though the lip adds drag that shows in the speed rating. On the 6204 bearing that is 10,000 RPM with 2RS seals against 16,000 RPM open or shielded.
How to Check a Hot Application Before You Order
Four checks tell you most of what you need. Do them with the machine running, or straight after a stop while the parts are still warm.
1Measure the housing at running temperature. A reading taken on a cold machine tells you nothing about the fit the bearing sees in service.
2Read the grease after a stop. Dark, hard or dry grease points at heat, and a dry raceway points at a grease that aged out early.
3Look at the cage. Discolored or loose pockets mean the cage has gone past its limit for that position.
4Measure the seat. A worn or galled seat changes the fit, and a changed fit changes the clearance you end up with.
Frequently Asked Questions
Why do bearings fail in ovens?
Heat closes the running clearance, ages the grease and softens a moulded cage. Most oven failures on a standard bearing come down to one of those three rather than a load problem.
Can I use a standard bearing in a hot position?
If the seat only runs warm, a standard bearing with fresh grease does the job. In a genuinely hot position you need a wider clearance group, a cage that survives the heat, a matched grease and the right seal.
Does a C3 clearance make a bearing noisy?
A C3 group is a normal build for a hot or heavily loaded position, not a defect. It only sounds loose when it is dropped into a cool, light position that never needed the extra gap.
Which cage should I ask for in heat?
Ask for a steel or brass cage once the seat runs past what a moulded polyamide cage can stand. The cage is usually the limit long before the steel is.
Will a hotter grease fix a hot bearing?
Only if the grease is the thing that failed. If the clearance has closed or the cage has softened, a better grease buys a little time and nothing more.
Application Review With Trial Parts
Send the temperature your equipment actually reaches at the bearing seat and the duty cycle, and we will name the clearance group, cage, grease and seal we would supply. Trial parts are available before a production run, so the choice can be proven on the machine. Yuanhe has 500+ B2B clients and 12,000+ OEM projects behind that work.
Request a quote and tell us what the position runs at.


Related Products